
Engine & Powertrain Component Machining
Powertrain components operate under high loads for thousands of hours. Their critical bores have to maintain that reliability.
Off-highway engines and drivetrains run at high load for years. Connecting rods, housings and gear components must hold micron-level tolerances across large volumes and a steady flow of variants. We build machining systems for exactly that: rotary table machines for high-volume parts, fine-boring machines for critical bores and machining centers for flexible lots.
Precision designed for long-term production stability.
From raw body to finished assembly.
One team answers for all of it.
Precision
Fine boring with non-overlapping feed axes holds diameter and position in the micron range.
Flexibility
Up to four part types run on one machine without retooling.
Throughput
Multi-spindle machining centers cut several parts in parallel. Output scales with the spindles, not the floor space.
Single Source
Rotary table, fine boring and machining center from one engineering team, matched to each other.
We deliver the system.
You operate it.
Precision Machining
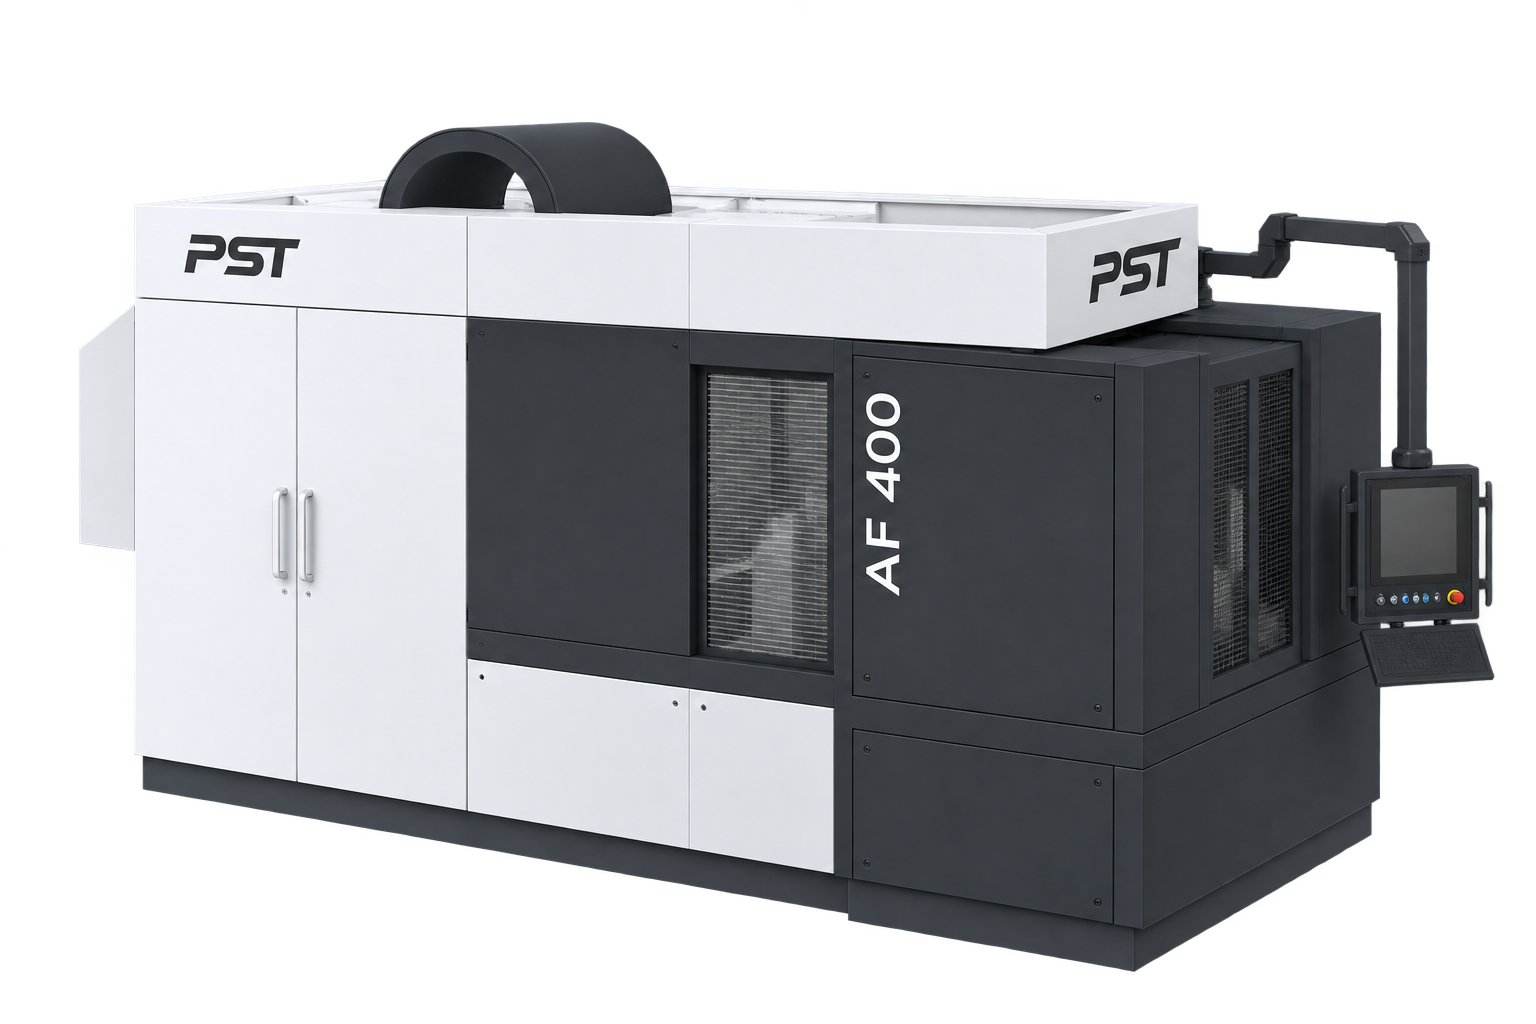
AF 400 Fine Boring Machine
A powertrain is only as durable as its critical bores. The AF 400 handles intermediate and fine boring in the micrometer range, bore after bore. Its feed axes are not stacked and its compact layout has no overhanging masses, which protects the geometry of every bore. A clamping cube lets you run up to four workpiece types without changeover. For large quantities there is the AR 400 Rotary Transfer Machine, for flexible lots the AC 400 Machining Center.
Discover Precision Machining at PST

Micrometers are not the goal, they are the starting point. Explore the machining systems that hold tolerances bore after bore, from high-volume production to flexible lots, and see how precision becomes routine.

Downloads
We send datasheets and technical documentation on request.
Custom Solutions & Retrofit
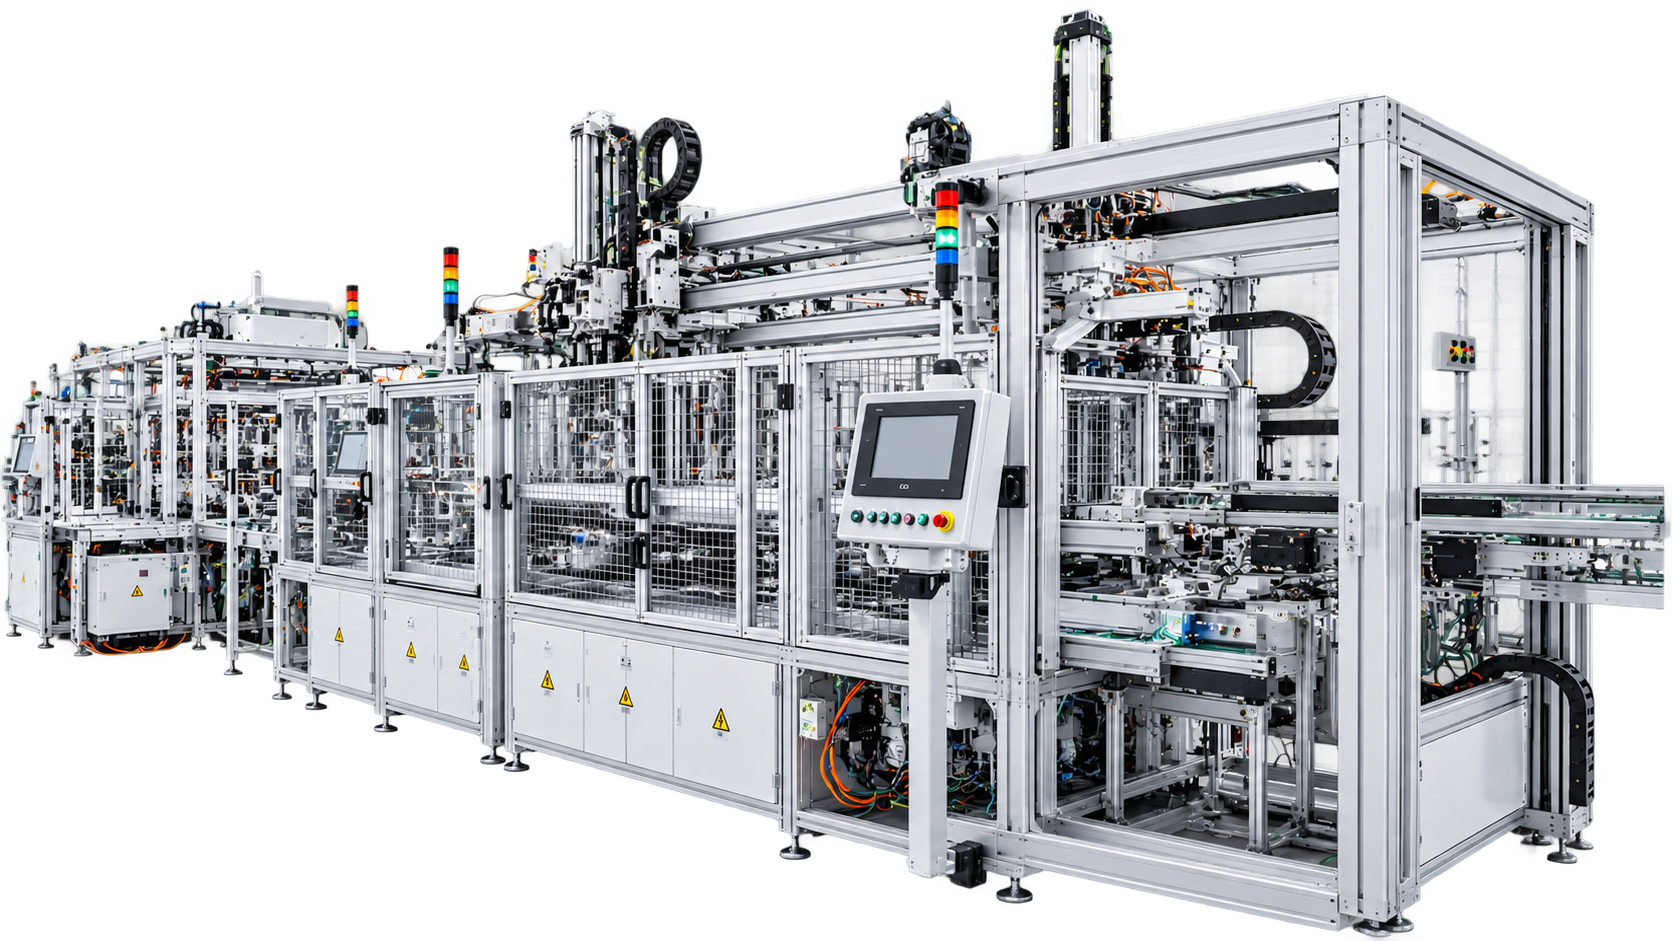
System Solutions
Machining does not stop at the machine. Every machine we build is also available as a turnkey system: different workpieces can run on the same line, you can expand in stages when volumes grow, and you get one system, delivered ready to run. For a process no standard machine offers, there are Custom Machines.
Discover Custom Solutions & Retrofit
Your process is not in a catalog, and your machine should not be either. Explore how we build, extend and modernize production systems around what you make, from the first sketch to the last shift.
Downloads
We send datasheets and technical documentation on request.
One team from first sketch to a line that runs.
A process that has proven itself. One team plans, engineers and commissions your machine, and hands it over turnkey, ready to run, in the shortest possible time.

Planning
Concept, material flow and scope, defined with you before the first drawing is released.

Engineering
Mechanics, controls and process, designed as one system and simulated before the build.
Realization
Build, installation and commissioning at your plant, then handed over ready to run.
Frequently Asked Questions
Can the AF 400 produce non-cylindrical bores?
Yes. Oval and trumpet-shaped bore profiles are produced with freely programmable geometry. Up to four workpiece types run on one machine without retooling.
Which parts suit the AR 400?
Medium-size parts that need several machining operations at high volume: housings, valve bodies, fittings, connecting rods and similar components.
How does the AR 400 keep cycle times short?
All stations machine at the same time, and parts are loaded in parallel with machining. The cycle time is set by the longest single operation plus indexing, not by the sum of all operations.
How many spindles does the AC 400 have?
2, 3, 4 or 5 motor spindles, with automatic tool change and tool magazine. Spindles with NC facing and additional spindle rows are available as options.
Can different part types share one AC 400?
Yes. Several workpiece types can run on one system, which keeps the investment productive across product families.
Still have questions? Get in touch with our support team and we'll
discuss your unique requirements.
Which tolerances can the AF 400 hold?
Bore diameters in the micrometer range, typically within ± 5 µm, with form and position held bore after bore. Non-stacked feed axes and no overhanging masses protect the geometry.
How does the AF 400 compensate tool wear?
An adjustment device in the fine boring spindles corrects the cutting edge position. Combined with post-process measurement, the machine keeps diameters inside tolerance automatically.
Which process capability do you design for?
Critical features are designed for a machine capability index (Cmk) of 1.67 or higher. We prove it in a documented capability study with your parts before the machine ships. Process capability (Cpk of 1.33 or higher) is then confirmed in series production on your floor.
Still have questions? Get in touch with our support team and we'll
discuss your unique requirements.
Can you test our parts before we place an order?
Yes. For critical joining, machining or inspection steps, we run feasibility trials with your sample parts. You see the result before you commit to the machine.
Which documentation do we receive with the machine?
Operating instructions, declaration of conformity, electrical and pneumatic schematics, spare parts lists and maintenance plans. PLC source code is supplied by agreement.
How long are spare parts available?
Every machine ships with a spare parts list and a recommended stock for your site. We keep wear parts available and support our machines with spare parts for at least ten years.
Still have questions? Get in touch with our support team and we'll
discuss your unique requirements.

Process System Technologies
Anton-Grimmer-Straße 4
73466 Lauchheim
Germany


